Key Learnings
Loosening and fatigue fracture are the dominant failure modes for wind‑turbine high‑strength bolts. Bolt reliability depends on full‑lifecycle control covering standards‑selection, material, manufacturing process, structural design and on‑site installation. Per ISO 898‑1 and DNV‑GL rules, wind‑turbine hardware shall adopt 8.8‑10.9 grades only; 12.9 and above are prohibited due to insufficient toughness. Existing general standards lack specifications for fatigue, corrosion‑resistance and extra‑large‑diameter bolts (≥M72).
| Dimension | Main technical points |
|---|---|
| Standard & mechanical requirements | 10.9‑grade: Rm ≥ 1040 MPa, Re ≥ 940 MPa; Charpy impact ≥27 J @‑20 °C (some low‑temp variants @‑40 °C). General standards omit fatigue, corrosion and large‑size bolt indexes, supplemented by group‑standards and purchaser‑supplier agreements. |
| Material selection | Medium‑low‑carbon alloy steel. Small‑size(≤M24):20MnTiB; medium(M27‑M33):35VB /35CrMoA; large‑size(≥M36):42CrMo,40CrNiMoA,B7. Improve metallurgical cleanliness and reduce inclusions to boost fatigue‑life. |
| Manufacturing process | ≤M36: cold‑heading workflow; large bolts: hot‑forging. Thread‑rolling must be done after quenching‑tempering to retain beneficial surface compressive residual‑stress. Corrosion coating: inland ≥720 h salt‑spray; offshore ≥1000 h salt‑spray; choose between hot‑dip‑galvanizing and Dacromet, watch coating‑process temperature impact on residual‑stress. |
| Structural design | Optimize bolt fillet and thread‑root by roll‑strengthening; or adjust connected‑part stiffness / shank‑diameter to mitigate alternating‑load amplitude, reduce stress concentration. Common types: hex‑head bolts, double‑end studs, anchor bolts. |
| Installation & preload control | Design preload for typical 10.9‑grade M36‑M45 bolts: 70‑80 % of yield strength. Adopt multi‑stage cross‑symmetrical tightening. Preload loss of 10‑20 % is defined as loosening‑failure. Avoid forced assembly, omitted washers, repeated disassembly and wrong torque. Use torque‑wrench / hydraulic tensioner plus anti‑loosening marking for inspection. |
Industry‑development trends
Simply enlarging bolt diameter has met practical limits. Future directions: upgrade material purity, optimize manufacturing processes, develop fatigue‑resistant ultra‑high‑strength bolts, complete dedicated wind‑fastener industry standards, and strengthen full‑lifecycle quality‑control for offshore wind large‑diameter fasteners.
In the wind power industry, high-strength bolts serve as critical components for reliable connections among core parts such as tower cylinders, blade roots, generators, and gearboxes. As single-turbine capacities continue to increase, applications for large-diameter, high-performance bolts are expanding.
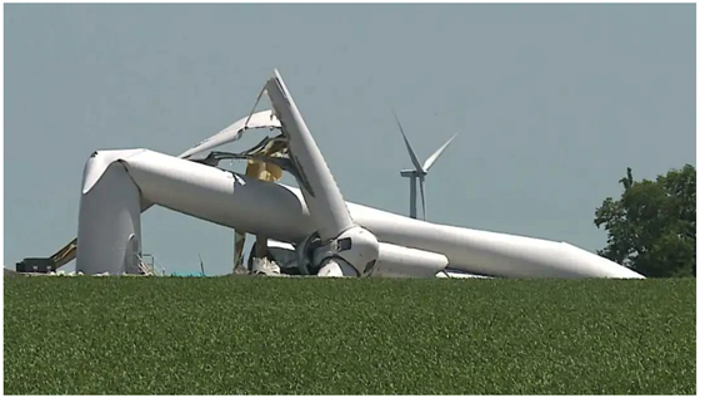
However, loosening and fatigue fracture remain the primary failure modes for wind turbine bolts. The performance of these bolts spans their entire lifecycle—from standard selection and material formulation to manufacturing, structural design, and on-site installation—each stage significantly impacting long-term service reliability.
I. Performance Standards for Wind Turbine Bolts
Within the industry, fasteners rated at 8.8 or higher are generally classified as high-strength bolts, with a minimum tensile strength of 800–830 MPa and yield strength equivalent to 80% of the tensile strength.
In wind power applications, bolt selection follows clear standards: according to ISO 898-1 and DNV GL guidelines, only high-strength bolts within the 8.8–10.9 grade range are permitted for securing wind turbine components. Bolts rated 12.9 and above are prohibited due to an imbalance between strength and toughness, which increases susceptibility to fatigue and cracking.
China’s current national standards GB/T 3098.1, GB/T 3098.8, and GB/T 3098.23—“Mechanical Properties of Fasteners”—clearly define specifications and fundamental mechanical properties for fasteners. The mainstream 10.9-grade bolts used in the wind industry are typically made from medium-to-low carbon alloy steel, processed through heat treatment modification and hot rolling to achieve required performance.
Key mechanical properties include a minimum yield strength of 940 MPa and a minimum tensile strength of 1040 MPa. Regarding low-temperature impact resistance, the Charpy V-notch impact energy must be no less than 27 J at -20°C; some low-temperature grades require this performance at -40°C.
However, existing general performance standards still have notable gaps. They do not specify corrosion resistance, fatigue resistance, or performance under elevated temperatures, nor do they define load requirements for extra-large diameter bolts (M72 and above).
These specialized performance criteria are often based on internal agreements between suppliers and customers or refer to group standards such as T/ZZB 0327-2018 “High-Strength Bolt Connections for Offshore Wind Power,” leading to inconsistencies in manufacturing processes and quality reliability across the fastener industry.
From an industry development perspective, simply increasing bolt diameter to enhance connection strength has reached its practical limit. Due to constraints in component design space and the inherent fatigue limitations of bolts themselves, further diameter increases are impractical.
Therefore, developing new materials, optimizing production processes, and creating fatigue-resistant ultra-high-strength 12.9-grade bolts represent the key future direction for wind turbine bolt technology.

II. Impact of Material Properties on Bolt Performance
High-strength bolts for wind power applications are typically manufactured from medium to low-carbon alloy steels (such as boron steel, manganese steel, and chromium steel), with carbon content generally controlled between 0.3% and 0.5%.
Subsequent heat treatment involving quenching and tempering is used to modify the material properties. Based on performance grade and material cleanliness, wind turbine bolt steels can be categorized into three types: ultra-clean bolt steel, non-tempered steel, and ultra-high-strength bolt steel. Among these, the hardenability of the material is a key factor determining the suitability of the bolt size.
Different bolt diameters require varying levels of material hardenability, and the industry has established well-defined material selection guidelines:
• For small-diameter bolts up to M24, 20MnTiB steel is commonly used, as its relatively low hardenability is sufficient to meet performance requirements;
• For medium-sized bolts ranging from M27 to M33, 35VB or 35CrMoA steel is typically selected;
• For large-diameter bolts of M36 and above, higher hardenability and superior overall performance are required, necessitating the use of grades such as 40CrNiMoA, 42CrMo, ASTM A193 B7 (American standard), or JIS G4053 SCM440 (Japanese standard). In applications requiring high low-temperature impact toughness, 40CrNiMoA steel is preferred. Nut materials are generally matched to the corresponding bolt material.
Currently, the wind power industry widely uses 42CrMo steel for large-scale bolts, whose manufacturing process is mature and stable, with controllable production costs and lead times. Industry research generally indicates that purifying the base material as much as possible, improving metallurgical cleanliness, and reducing internal inclusions and defects are fundamental measures to ensure bolt performance and enhance fatigue life.

III. Impact of Manufacturing Process on Bolt Performance
The manufacturing process for wind power high-strength bolts is divided into two types based on raw material form and bolt specifications, with the core difference lying in the forming method:
• Cold Heading Process: Suitable for bolts up to M36, with a complete production route including hot-rolled wire rod → spheroidizing annealing → pickling and phosphating → drawing → cutting → cold heading → heat treatment (quenching and tempering) → thread rolling → non-destructive testing → cleaning → shot blasting → surface treatment.
The cold heading process offers higher material utilization and production efficiency; however, spheroidizing annealing must be performed prior to processing to improve material ductility and ensure forming quality.
• Hot forging process: Suitable for large-sized bolts. The complete production route is hot-rolled bar → pickling and phosphating → drawing → cutting → hot forging → machining and shaping → heat treatment (quenching and tempering) → thread rolling → non-destructive testing → cleaning → shot blasting → surface treatment.
Thread processing is a critical step affecting bolt fatigue performance. Industry consensus holds that thread processing should be performed after heat treatment, with priority given to one-time roll-forming processes over machining by turning.
This method generates appropriate residual compressive stress on the thread surface while minimizing microcracks and sharp-edge defects introduced during mechanical processing. If rolling is performed before heat treatment, the surface residual compressive stress will dissipate, significantly weakening the bolt’s fatigue performance.
Surface corrosion protection is another key stage in wind turbine bolt manufacturing, with process selection directly influencing the bolt’s corrosion resistance and fatigue life. Based on the application environment of the turbine unit, corrosion requirements are divided into two levels: inland units require fasteners to pass a salt spray test for at least 720 hours without red rust on the substrate; offshore units require more than 1,000 hours of salt spray testing without red rust on the substrate.
The mainstream corrosion protection processes in the industry are hot-dip galvanizing and Dacromet coating, which differ significantly in performance:
• Hot-dip galvanizing is carried out at temperatures between 450°C and 480°C. The resulting passivation layer may contain crystalline water, limiting high-temperature performance.
• Dacromet is a zinc-chromium coating applied at approximately 280°C. It forms a dense film with low moisture content, offering both cathodic protection and barrier effects, providing superior corrosion and high-temperature resistance. However, it has relatively lower wear resistance and long-term atmospheric corrosion resistance.
It should be noted that the processing temperatures for different surface treatments vary significantly. High temperatures can cause residual stresses on the bolt surface to dissipate, thereby deteriorating fatigue life; therefore, surface treatment parameters must be optimized according to operational requirements.

IV. Impact of Structural Design on Bolt Performance
Common bolt types used in the wind power industry include hex head bolts, double-ended studs, and anchor bolts. Both the bolt’s own structure and the design of the connected components directly affect the bolt’s service performance and lifespan.
From the perspective of the bolt’s own structure, dimensions, thread length, and thread profile parameters significantly influence bolt life, with national standards specifying strict dimensional requirements. Structural reinforcement at critical areas of the bolt has been proven effective in extending service life—for example, applying roll-forming strengthening to the fillet regions or using graded thread rolling processes can enhance fatigue resistance by introducing residual compressive stresses and optimizing stress distribution.
In engineering design, beyond optimizing the bolt’s own structure, designers often prefer to improve connection reliability by modifying the structure of the connected components: on one hand, increasing the overall stiffness of the connected parts reduces the amplitude of alternating loads experienced by the bolt; on the other hand, reasonably reducing the shank diameter within acceptable limits—thereby lowering the bolt’s inherent stiffness—can also optimize stress distribution and extend fatigue life.
V. Impact of Installation Practices on Bolt Performance
Installation is the stage in a bolt’s lifecycle most prone to human-induced deviations, with installation clearance control, operational compliance, and product integrity directly affecting the bolt’s actual service life.
In real-world installations, several non-compliant practices frequently occur: forced installation or removal due to insufficient clearance; lack of understanding by installers regarding bolt design leading to missing transport protection, omitted washers, incorrect bolt orientation, or repeated disassembly; and in some cases, inadequate tightening torque or insufficient anti-loosening measures.
These defects can directly damage the bolt’s surface coating and cause abnormal thread deformation, triggering premature loosening and subsequently accelerating corrosion and fatigue failure.
Control of preload is the key indicator of installation quality. For 10.9-grade M36–M45 high-strength bolts commonly used in wind power applications, the designed preload typically ranges from 70% to 80% of the standard yield strength. The effectiveness of preload application is influenced by multiple factors: elastic interaction with adjacent bolts and washer creep relaxation both reduce initial preload. Employing a three-stage cross-tightening process can effectively minimize this loss of initial preload.
Currently, there is no unified industry standard for determining bolt loosening. Based on research findings for smaller-sized bolts, a general consensus holds that when the actual preload drops by 10%–20%, the bolt is considered to have failed due to loosening.
Loosening is often accompanied by observable signs: relative displacement of anti-loosening marking lines, gaps appearing in the fastened structure, wear of the thread surface coating (or even exposure of the base material), and circumferential sliding wear marks on the thread surface.
On-site engineering typically uses torque wrenches or hydraulic tensioners for preload installation. To ensure preload reliability, anti-loosening washers or double nuts are often added, while anti-loosening marking lines are applied to facilitate quick inspection of bolt looseness during maintenance operations.

VI. Conclusion
The reliability of high-strength bolts for wind power is the fundamental guarantee for the long-term stable operation of wind turbine units. Their performance is not determined by a single factor, but rather results from the combined effects of materials, manufacturing processes, design, and installation throughout the entire lifecycle.
As wind power capacity continues to grow toward larger scales and deeper offshore deployment, requirements for bolt performance will keep increasing. Therefore, refining industry standards, standardizing full-process control, and deepening research on large-diameter bolt performance represent the core development directions for the industry in the future.
If you are looking for suitable bolts and nuts, please visit us here https://hktl-fastener.com/bolts-and-nuts/.