Key Findings
Bolt overload fracture happens when axial load exceeds bolt‑rated strength, mostly initiating in the threaded section. Visible necking varies across strength grades but cannot serve as sole judgement evidence. Verify core hardness per GB/T3098.1 for neck‑showing fractures; 12.9‑grade failures require metallographic examination. Root causes include over‑torquing, cumulative preload‑plus‑working‑load stress and improper design sizing. Prevention covers torque management, avoidance of eccentric bending, correct material‑grade selection, anti‑loosening, quality control and routine maintenance.
| Strength Grade | Overload‑fracture Necking Feature | Identification Method |
|---|---|---|
| 8.8 | Obvious necking | Test core hardness conforming to GB/T3098.1 |
| 10.9 | Moderate / slight necking | Test core hardness conforming to GB/T3098.1 |
| 12.9 | Almost no necking | Metallographic fracture‑surface analysis mandatory |
Overload‑fracture root causes: excessive installation torque creating excessive pre‑load; pre‑load plus superimposed operational working load exceeding bolt capacity; insufficient bolt nominal diameter or improper strength‑grade in design. Note necking can also stem from poor material / inadequate heat‑treatment, not purely overload.
Preventive measures:
- Torque control: Use calibrated torque wrenches; account for lubrication effect; adopt turn‑of‑nut or hydraulic tensioner for critical bolts; avoid uncontrolled pneumatic‑wrench tightening.
- Eliminate extra stress: Keep joint surfaces flat, prevent eccentric / bending / shear loading; avoid threads sitting within shear planes.
- Correct selection: Match strength grade, diameter and thread length; use fillet‑transition bolts to mitigate stress concentration.
- Anti‑loosening: Apply locking devices to stop loosening‑induced impact overload; guarantee even load distribution on bolt groups.
- Material‑process quality: Reject defective bolts; implement dehydrogenation for high‑strength bolts; limit repeated disassembly to protect threads.
- Maintenance: Inspect for elongation, crack and corrosion; replace damaged bolts; prohibit impact start‑stop and overload operation.
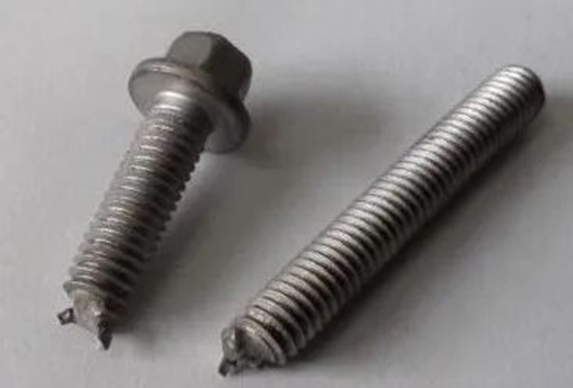
During service, the hazard of bolt fracture is extremely high, being the most fatal form of failure in fastening connections. There are many reasons for bolt fracture. Today, let’s talk about overload fracture.
I. What is bolt overload fracture?
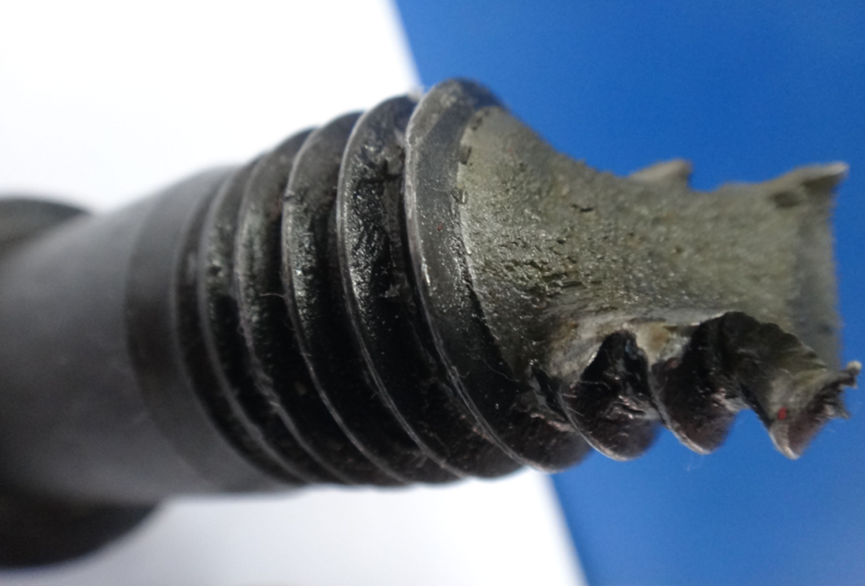
Bolt overload fracture refers to the fracture of a bolt when the axial load it bears exceeds the load it is allowed to bear according to its strength. Due to the small stress area at the bolt thread, the stress there is greater than that at the bolt shank, so overload fractures usually occur at the thread.
Bolts of different strength grades show different appearances when they are overloaded and fractured. The fracture of an 8.8 grade bolt will have a distinct necking phenomenon; the fracture of a 10.9 grade bolt will also have a certain degree of necking, but not as obvious as that of the 8.8 grade; while a 12.9 grade bolt will hardly show any necking at all.
However, the presence of a necking phenomenon does not necessarily indicate that the bolt has undergone overload fracture. Because if bolts from 8.8 grade to 12.9 grade are made of improper materials or undergo improper heat treatment, resulting in the core hardness not meeting the standard after quenching and causing the bolt to break, the fracture surface will also show a necking phenomenon.
II. How to Determine if a Bolt Fracture is Due to Overload?
Necking cannot be used as a basis for determining whether a bolt fracture is caused by overload. To determine if a bolt has fractured due to overload, further analysis is required.
For fractures with a necking phenomenon, samples need to be taken from the fractured bolt, and the core hardness of the bolt should be tested and judged in accordance with the requirements of GB/T3098.1. Only if it is qualified can it be determined that the bolt fracture is due to overload.
For 12.9 grade bolts that fracture due to overload, there is no necking phenomenon. The fracture may be caused by surface defects and material defects in the threaded area. Therefore, only through metallographic analysis of the fracture surface can it be determined whether it is an overload fracture.
III. What are the causes of bolt overload fracture?
Now that we know how to identify overload fracture, let’s talk about the possible causes of it. As mentioned earlier, overload fracture occurs in bolt connections subjected to axial loads. The possible causes are as follows:
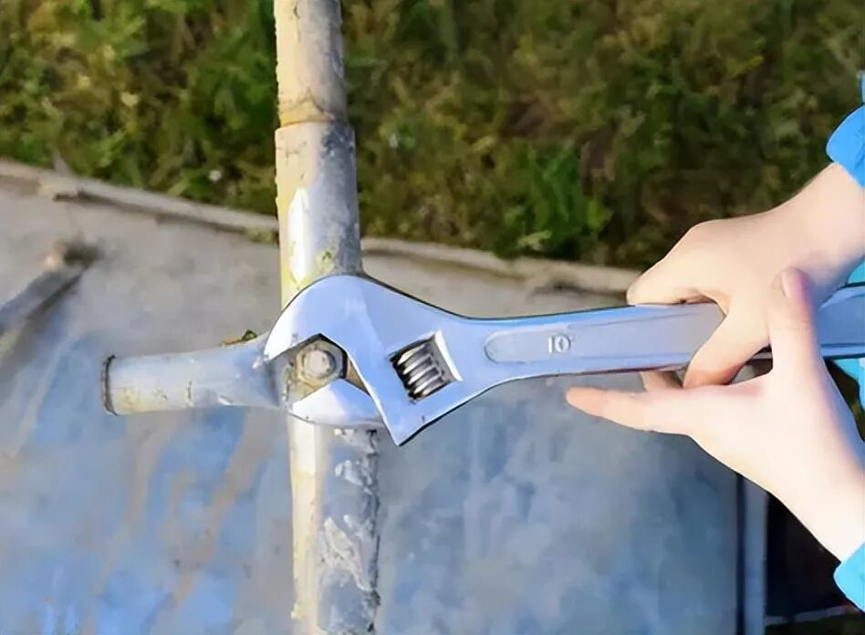
If the torque applied during bolt installation is too large, the preload exceeds the bolt’s strength, resulting in overload fracture.
Also, if the torque applied during installation is too large, the preload approaches the bolt’s strength. However, during the operation of the equipment, the bolt has to bear not only the residual preload but also the working load of the mechanical equipment. If the sum of these two forces exceeds the bolt’s strength, it will also lead to overload fracture.
In addition, if the nominal diameter of the bolt thread is not properly selected during design, it can also cause bolt overload fracture.
Note: The magnitude of the residual preload is directly proportional to the preload.
IV. Methods to Prevent Bolt Overload Fracture
1. Control the tightening torque to prevent overload at the source
Tighten strictly according to the design torque, use a torque wrench / torque coefficient control.
Avoid excessive torque and random tightening with pneumatic wrenches.
Use uniform lubrication: torque differs with or without lubrication; do not estimate roughly by dry tightening.
For critical bolts, use the turn-of-nut method or hydraulic tensioner, which is more stable than pure torque control.
2. Avoid additional bending moment, shear and eccentric loading
Ensure flatness of connected parts, no warping or forced alignment.
Keep gaskets flat, non-inclined and non-suspended.
Install bolts centrally, without prying or forced misalignment.
Do not let threads enter the shear plane.
3. Select correctly to ensure strength and structure
Select the strength grade (8.8, 10.9, 12.9, etc.) according to working conditions; do not use lower-grade substitutes.
Ensure sufficient diameter, length and thread length.
Prefer bolts with fillets and reduced shank bolts to reduce stress concentration.
Use heat-resistant and corrosion-resistant bolts in high-temperature / corrosive environments to avoid section reduction.
4. Reduce impact, vibration and alternating loads
Apply locking measures: spring washers, all-metal locking washers, double nuts, thread locking adhesive.
Loosening causes impact overload, so locking equals overload prevention.
Use bolt groups with sufficient preload for high-vibration parts to ensure even load distribution.
5. Control material and processing quality
Do not use bolts with cracks, inclusions or poor heat treatment.
Prevent hydrogen embrittlement (especially critical for high-strength bolts, requiring hydrogen control and dehydrogenation treatment).
Avoid excessive repeated disassembly and assembly to prevent thread damage.
6. Operation and maintenance
Regularly inspect looseness, elongation, deformation and corrosion.
Replace bolts that are stretched, stripped or cracked; do not use them temporarily.
Strictly prohibit overload operation and impact start-stop.
If you are looking for suitable bolts and nuts, please visit us here https://hktl-fastener.com/bolts-and-nuts/.